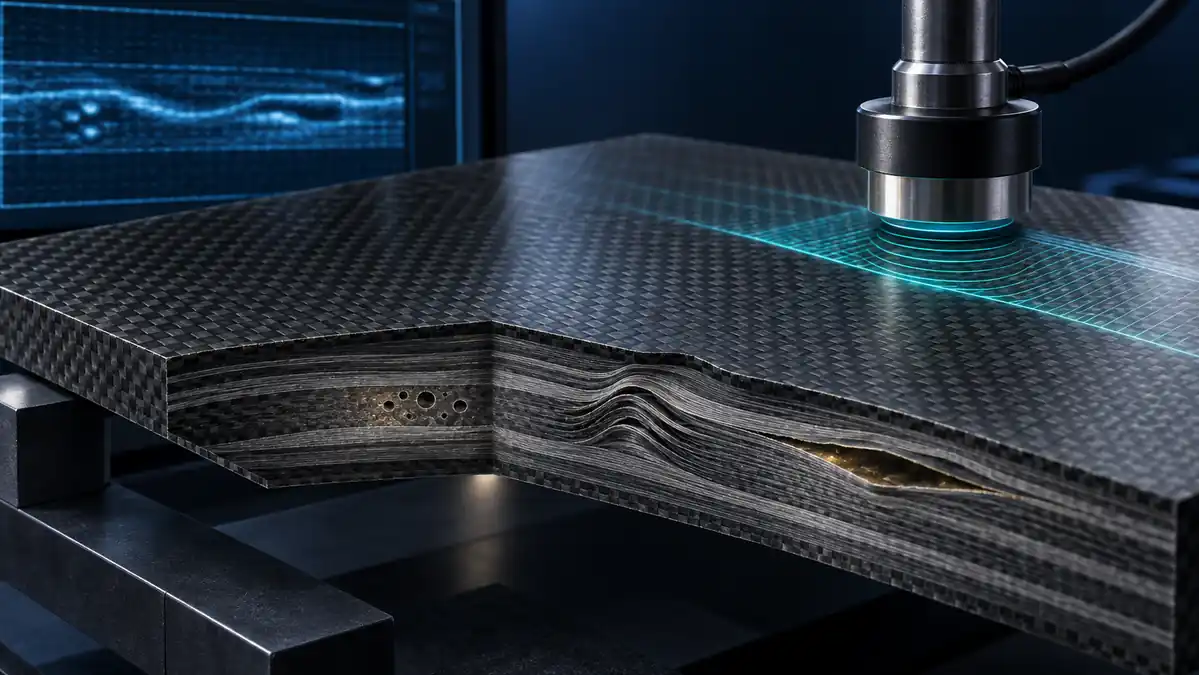
Carbon fiber layup design converts real loads into fiber directions, ply types, stacking order, thickness, and local reinforcement. A carbon part is not equally strong in every direction: 0° plies primarily carry axial loads, ±45° plies carry in-plane shear and torsion, and 90° plies support transverse loads and dimensional stability. The best laminate places enough fiber along each load path while remaining manufacturable, inspectable, and damage tolerant.
This guide is for engineers, product developers, and sourcing teams preparing a custom carbon fiber component. It explains the design language needed for a productive DFM and quotation review. The Carbon Fiber Layup shown are teaching examples—not approved ply schedules for a specific part.
Carbon Fiber Layup Design at a Glance
| Orientation or feature | Primary contribution | Typical use | Important limitation |
|---|---|---|---|
| 0° plies | Axial stiffness and strength | Beams, tubes, shafts, long load paths | Do little for unsupported transverse or shear loads |
| +45° / -45° plies | In-plane shear and torsion | Torque tubes, webs, shells, load transfer around features | Usually need both signs to avoid imbalance |
| 90° plies | Transverse stiffness, splitting resistance, dimensional support | Hoop direction, wide panels, transverse loads | Not a substitute for adequate 0° load-carrying fiber |
| Unidirectional (UD) | Efficient directional properties | Primary structural load paths | Requires deliberate off-axis and handling support |
| Woven fabric | Two-direction reinforcement, drape and surface stability | Complex skins and cosmetic outer plies | Fiber crimp reduces directional efficiency |
| Balanced laminate | Pairs +θ and -θ plies | Reducing extension-shear coupling | Balanced does not automatically mean symmetric |
| Symmetric laminate | Mirrors plies around the mid-plane | Reducing extension-bending coupling and cure distortion | May add plies beyond a single load requirement |
| Quasi-isotropic laminate | Similar in-plane behavior in multiple directions | Multi-directional panels and uncertain load paths | Not truly isotropic and often less mass-efficient than a tailored layup |
The table is a starting vocabulary, not a design recipe. Final performance depends on fiber grade, resin, fiber volume, cure, defects, geometry, joints, environment, and the interaction among all plies. Our articles on carbon fiber modulus and T700 carbon fiber explain why material designation alone does not define part performance.
Start With Load Paths, Not a Familiar Ply Schedule
A common mistake is copying a laminate such as [0/90/±45]s because it looks complete. A better process begins with how load enters, travels through, and leaves the component.
Document at least these cases:
- axial tension and compression;
- bending direction and allowable deflection;
- torsion and in-plane shear;
- buckling of thin skins, webs, or tubes;
- fatigue spectrum and load reversals;
- impact, dropped-tool, crash, or rough-handling events;
- loads introduced through bolts, inserts, adhesive joints, or clamps;
- thermal and moisture cycles that can create residual stresses.
A part may have excellent axial coupon strength yet fail at a hole because the bearing and bypass loads were not supported. It may resist static bending but twist excessively because it lacks ±45° reinforcement. It may pass the first load test but crack at a thickness transition during fatigue. The dominant failure mode—not the largest published fiber number—should drive the Carbon Fiber Layup.

What Do 0°, 45°, and 90° Mean?
The designer establishes a reference direction, normally tied to a primary axis or drawing datum. A 0° ply runs along that reference. A 90° ply runs across it. +45° and -45° plies run diagonally in opposite directions.
0°: axial load and bending stiffness
In a long beam, paddle shaft, mast, or robotic arm, 0° fibers usually carry much of the axial tension and compression. When placed away from the laminate mid-plane, axial plies can contribute strongly to bending stiffness. However, adding only 0° material can leave the laminate vulnerable to splitting, shear, handling damage, and loads around joints.
±45°: shear transfer and torsion
Off-axis fibers are critical in torque tubes, closed sections, webs, and shells. Under torsion, the principal load paths commonly run diagonally, so +45° and -45° reinforcement can be more effective than additional axial fiber. Pairing positive and negative angles also helps avoid an unbalanced laminate that deforms in an unintended coupled mode.
90°: transverse support and hoop direction
Ninety-degree plies can carry transverse loads, help resist longitudinal splitting, stabilize width, and support fastener or pressure loads. In a tube, what is called 90° relative to the tube axis becomes a circumferential or hoop direction. The functional meaning therefore depends on the drawing coordinate system.
Other angles can be correct
Angles are not limited to 0°, ±45°, and 90°. A helical tube, swept structure, pressure vessel, or complex shell may benefit from other orientations. Manufacturing repeatability, cutting waste, steering limits, drape, and inspection must be considered before specifying unusual angles.

Unidirectional vs Woven Carbon Fiber
Carbon fiber material is supplied in several reinforcement forms. The choice affects structural efficiency and how reliably a shop can place the fibers.
Unidirectional tape and fabric
UD reinforcement puts most fibers in one direction, making it efficient for a known load path. Designers can build a tailored laminate by placing separate 0°, ±45°, 90°, or other-angle plies. UD is valuable when mass and stiffness are tightly controlled, but it requires careful ply handling, orientation identification, edge support, and off-axis reinforcement.
Woven fabric
A woven fabric contains fibers in two principal directions and is easier to handle as a stable sheet. It can drape over contours and provide a consistent cosmetic pattern. Because yarns pass over and under one another, crimp reduces the straight-fiber efficiency compared with an equivalent UD architecture. Woven outer plies may improve handling and surface stability, but a cosmetic twill layer should not be assumed to carry the primary structural load.
Biaxial and multiaxial non-crimp fabrics
Stitched non-crimp fabrics can combine 0°/90° or ±45° layers without conventional weaving crimp. They are useful in infusion and larger structures, although stitching, bulk, permeability, drape, and resin flow affect the finished laminate.
Chopped-fiber charge materials
Chopped carbon charge formats can fill complex compression-molded geometry and support higher production rates. They do not provide the same continuous, controllable load paths as UD tape. A compression molding DFM should therefore distinguish continuous prepreg, sheet molding compounds, and chopped-fiber charge systems rather than treating them as one material.
Balanced, Symmetric, Cross-Ply, and Quasi-Isotropic Carbon Fiber Layups
Laminate shorthand is useful only when the reference axis, material, ply order, and notation are unambiguous.
Balanced laminates
A balanced laminate contains a +θ ply for each corresponding -θ ply of the same material and thickness. This can reduce coupling between normal extension and in-plane shear. For example, +45° and -45° plies commonly appear as a pair.
Symmetric laminates
A symmetric laminate mirrors its stacking sequence around the mid-plane. Symmetry can reduce extension-bending coupling and help control warpage, but cure gradients, tool interaction, geometry, resin shrinkage, and uneven features can still distort a real part.
Cross-ply and angle-ply laminates
Cross-ply laminates primarily combine 0° and 90° plies. Angle-ply laminates use positive and negative off-axis orientations such as ±45°. Real parts often use a combination based on axial, transverse, and shear requirements.
Quasi-isotropic laminates
A quasi-isotropic laminate uses multiple orientations to approximate similar in-plane properties in several directions. It can be practical for panels with multi-directional or uncertain loads. It is not isotropic through the thickness, and its strength, joints, damage behavior, and bending response remain laminate-specific. If loads are well known, a tailored laminate may meet the requirement with less mass.
NASA’s Basic Mechanics of Laminated Composite Plates provides a deeper treatment of laminate stiffness and coupling. Engineering analysis should be performed by qualified personnel for structural or safety-critical components.
Why Ply Order Matters
Two laminates can contain the same count of 0°, ±45°, and 90° plies yet behave differently because the stacking sequence changes where each ply sits through the thickness.
- Bending: plies farther from the mid-plane have greater leverage in bending.
- Surface durability: outer plies experience handling, abrasion, impact, UV, and finish requirements.
- Interlaminar stress: abrupt stiffness changes and free edges can raise through-thickness stresses.
- Damage containment: ply order influences matrix cracking, delamination, and how damage progresses.
- Manufacturing: small cut pieces, bridging-prone plies, and unstable first plies can reduce repeatability.
- Cosmetics: a visible weave direction and print-through requirement may affect the outer stack without defining the structural core.
For sandwich panels, the facesheets carry much of the bending load while the core separates them and carries shear. Facesheet orientation, core density, adhesive film, edge closeouts, inserts, and local crushing must be designed as a system.

Designing Around Holes, Inserts, and Thickness Changes
Fastener holes and bearing loads
A drilled hole cuts load-carrying fibers and concentrates stress. The joint may be governed by bearing, net tension, shear-out, pull-through, or delamination. Local reinforcement, larger load-spreading hardware, controlled drilling, edge distance, and a suitable stacking sequence can be more important than simply increasing global thickness.
Bonded inserts
Define insert material, isolation, surface preparation, bondline, load direction, installation datum, and inspection. Carbon fiber is electrically conductive, so contact with aluminum in moisture may require galvanic isolation.
Drop-offs and transitions
Stopping several plies at the same line creates a sharp stiffness discontinuity. Staggered ply drop-offs, adequate taper length, continuous cover plies, and manufacturing access may reduce interlaminar stress. Exact rules depend on materials, thickness, load, and qualification basis.
Radii and corners
Tight inside radii can cause bridging, wrinkles, resin-rich pockets, fiber distortion, or tool-release problems. Outside corners may thin or open the weave. DFM should review radius, draft, split lines, ply splices, compaction access, and trimming allowances before tooling.
Match the Layup to the Manufacturing Process
A laminate that is analytically attractive may be slow, error-prone, or impossible to build. Noah Composites reviews the Carbon Fiber Layup within the full carbon fiber manufacturing route.
Prepreg and autoclave
Prepreg supports controlled resin content and accurate ply kits. Autoclave manufacturing adds heat and pressure for consolidation. Ply count, debulk stages, storage exposure, splices, release strategy, and cure tooling affect repeatability. For the production sequence, see how prepreg carbon fiber parts are made.
Infusion and RTM
Dry stacks must allow resin to reach all regions without disturbing fiber orientation. Fabric permeability, stack thickness, race tracking, flow media, preform stability, and vents become design inputs. A theoretically optimized stack that cannot be infused consistently is not production ready.
Compression molding
Matched tooling can support repeatable geometry and shorter cycles. Continuous plies may shift as the tool closes; chopped charge can flow but creates a distribution of fiber orientations. Charge pattern, closing direction, ribs, bosses, knit lines, and trimming must be considered with the structural requirement.
CNC trimming and drilling
Final datums, holes, and edges often require carbon fiber CNC machining. The drawing should distinguish as-molded and machined features. Specify critical datums, edge finish, breakout limits, dust control expectations, and inspection method rather than applying metal tolerances to every composite surface.
Common Carbon Fiber Layup Design Mistakes
- Designing the shape as if it were metal. Composite load paths, joints, and thickness transitions need purpose-built geometry.
- Using fiber datasheet values as finished-part allowables. Laminate and part properties are lower and depend on process and defects.
- Adding only 0° plies. This may improve axial stiffness while leaving shear, splitting, torsion, and joints weak.
- Calling every multi-angle stack quasi-isotropic. Orientation proportions, symmetry, repetition, and material equality matter.
- Ignoring compression and buckling. A thin laminate can buckle before reaching coupon strength.
- Using a woven cosmetic skin as proof of structure. Appearance does not reveal internal fiber architecture or quality.
- Specifying angles without a datum. A 0° note is meaningless unless the drawing defines the reference direction.
- Over-specifying a proprietary ply schedule too early. Define functional requirements and allow DFM review before freezing details.
- Skipping representative testing. Flat coupons may not capture corners, joints, holes, inserts, curvature, or process scale-up.
How to Specify a Layup in a Drawing or RFQ
A useful request package separates required outcomes from proposed construction. Include:
- 3D CAD and a controlled 2D drawing with revision;
- the coordinate system and 0° reference direction;
- load cases, boundary conditions, allowable deflection, fatigue life, and safety factors;
- service temperature, moisture, chemicals, UV, fire, impact, electrical, and RF conditions;
- maximum mass, envelope, nominal thickness, and permitted local buildups;
- material system or required property envelope;
- critical interfaces, holes, inserts, bonds, and no-splice zones;
- cosmetic faces, weave direction, gloss, color, and surface acceptance limits;
- prototype and annual quantities, target cost, and schedule;
- inspection, traceability, coupon, first-article, and proof-test requirements;
- which details the supplier may optimize during DFM.
The FAA’s AC 21-26A quality-system guidance for composite structures emphasizes documented control of materials and manufacturing processes. Although written for aviation, the principle is broadly useful: repeatable composite performance requires controlled inputs, process records, inspection, and change management.

Validation: From Coupon to Representative Part
Validation should match project risk. A staged plan may include:
- Material screening: supplier data, cure trials, and basic physical properties.
- Laminate coupons: tension, compression, shear, flexure, open-hole, bearing, impact, fatigue, or environmental conditioning as relevant.
- Subcomponents: joints, inserts, corners, sandwich closeouts, and thickness transitions.
- First articles: dimensional inspection, mass, finish, cure records, and nondestructive evaluation where appropriate.
- Representative component tests: proof, ultimate, fatigue, impact, thermal, vibration, or field-use tests.
ASTM composite standards include methods for tension, compression, shear, flexure, fatigue, moisture conditioning, glass-transition temperature, and other properties. ASTM D3039/D3039M covers in-plane tensile properties, but no single coupon test qualifies an entire component.
FAA AC 20-107B on composite aircraft structure describes the need to address environment, variability, damage, manufacturing defects, and substantiation. Requirements for non-aviation products differ, but the evidence-based mindset remains valuable.
A Practical Layup Development Workflow
- Define use conditions, coordinate system, interfaces, and failure criteria.
- Map load paths for each critical load case.
- Allocate 0°, off-axis, and transverse reinforcement to those paths.
- Select UD, woven, multiaxial, chopped, core, and resin formats.
- Develop a balanced and/or symmetric baseline where appropriate.
- Review buckling, joints, holes, impact, fatigue, and environment.
- Run manufacturing DFM for drape, seams, debulk, resin flow, tooling, cure, and trim.
- Analyze the laminate and geometry with project-appropriate methods.
- Build coupons, subcomponents, and first articles.
- Freeze the approved drawing, ply book, inspection plan, and change-control process.
Noah Composites supports this transition through research and development, tooling, prototyping, molding, machining, and inspection. The customer remains responsible for defining application requirements and approving the final validation basis.
Frequently Asked Questions
What is the strongest carbon fiber orientation?
Fibers are most efficient along their own axis, but a part rarely experiences only one load direction. The best orientation is the one aligned with each critical load path while other plies support shear, transverse loads, joints, stability, and damage tolerance.
What does a [0/45/-45/90]s layup mean?
It describes a sequence of four orientations mirrored about the laminate mid-plane; the “s” indicates symmetry. The notation is incomplete unless material, ply thickness, reference direction, repetition, surface order, and any special rules are also defined.
Is quasi-isotropic carbon fiber equally strong in every direction?
No. It approximates similar in-plane elastic behavior in selected directions. It is not isotropic through the thickness, and strength, joints, bending, impact, and damage remain dependent on the actual stack and geometry.
Is unidirectional carbon fiber stronger than woven carbon fiber?
UD is usually more efficient in its primary direction because its fibers are straight and concentrated. Woven fabric provides two-direction reinforcement, handling stability, drape, and cosmetic consistency. The better choice depends on load path, geometry, process, and inspection needs.
Should every carbon laminate be symmetric and balanced?
These are valuable design strategies, not universal laws. Some optimized or geometrically constrained laminates may be intentionally unsymmetric or unbalanced, but the resulting coupling, distortion, and manufacturing risks must be analyzed and validated.
Can a supplier design the ply schedule from a CAD model?
A CAD model defines geometry, not loads or acceptance criteria. A responsible design review also needs boundary conditions, load cases, environment, allowable deformation, life, safety factors, interfaces, quantity, and validation requirements.
Build a Manufacturable Carbon Fiber Laminate
Good carbon fiber layup design is a controlled allocation of material—not a contest to add the most carbon. Fiber orientation follows load paths; stacking order manages bending, coupling, damage, and manufacturing; local details protect the places where real parts often fail.
For a drawing-based DFM and quotation review, see our custom composite products capabilities or contact Noah Composites. Share the application, drawings, loads, environment, quantities, and validation expectations so the material and manufacturing route can be reviewed together.